Steam & Condensate recovery Liquid drainer (air trap) Fluid control Flow meter Heat pump system Safety valve Ancillary products Intelligent monitoring systems Hot water system Humidifier
Hospital Applications Hydrogen Refueling Stations & Hydrogen Pipeline Applications Application
Pamphlet/Catalog Download Technical article Frequently Asked Questions News
●Armstrong Humidification Solutions deliver comprehensive humidity control technologies, including Steam, Gas, Electric, and Atomization humidification systems for commercial buildings and industrial process applications. Designed to provide precise humidity control, these solutions improve indoor air quality, protect sensitive manufacturing processes, and enhance occupant comfort across a wide range of industries.
●The Armstrong 9000 Series Steam Humidifier conditions steam before it enters the airstream through four critical processes: filtration, steam-water separation, drying, and noise attenuation. This unique steam conditioning technology produces high-quality dry steam, reduces condensate formation, improves humidification efficiency, and minimizes maintenance requirements. The 90 Series Humidifier integrates a steam separator, dispersion tube, and steam trap into a complete humidification assembly for AHUs and duct systems, providing reliable humidity control for HVAC systems, hospitals, pharmaceutical and biotechnology facilities, food processing, electronics manufacturing, semiconductor plants, data centers, museums, and cleanroom environments.
●AVS is a Finnish industrial valve manufacturer recognized for Nordic engineering, reliable performance, and durable flow control solutions. Designed to meet the demands of industrial applications, AVS valves are widely used in water treatment, HVAC, energy, pulp and paper, chemical processing, and general industrial systems.
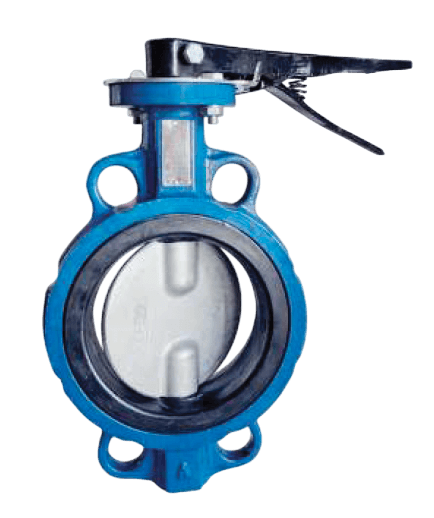
●The AVS SK Series Rubber Lined Butterfly Valve features a wafer-type full-port design with gas- and vacuum-tight sealing performance. Its interchangeable resilient seat provides excellent sealing, simplified maintenance, and extended service life. Available with manual, gear-operated, pneumatic, electric, or hydraulic actuation, the SK Series delivers dependable isolation and flow control for a wide range of industrial applications.
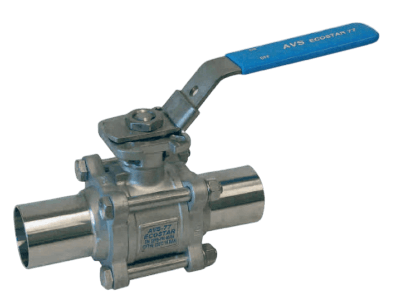
●AVS is a Finnish industrial valve manufacturer renowned for Nordic engineering, premium quality, and dependable flow control solutions. Designed for demanding industrial environments, AVS Ball Valves deliver outstanding sealing performance, durability, and long service life across a wide range of process applications.
●The AVS Ball Valve portfolio includes the Ecostar 77 Three-Piece High Performance Ball Valve and the Series 725000 Full-Bore Wafer Ball Valve. Key features include full-bore construction, ISO 5211 actuator mounting pads, blow-out proof stems, antistatic devices, and PTFE sealing technology, supporting manual, pneumatic, and electric actuation. These valves are ideal for chemical processing, petrochemical plants, water treatment, food and beverage production, pharmaceutical manufacturing, HVAC systems, energy facilities, and general industrial flow control.
●The Armstrong 2000 Series Stainless Steel Inverted Bucket Steam Trap is engineered to deliver dependable condensate removal and long-term performance in demanding steam applications. Combining Armstrong's proven inverted bucket operating principle with a full 304 stainless steel construction, the 2000 Series minimizes live steam loss while providing exceptional corrosion resistance, water hammer resistance, and extended service life.
●Designed for simplified installation and maintenance, the trap can be paired with the IS-2 Universal Connector, allowing rapid replacement without removing the piping assembly. Rated for operating pressures up to 4.5 MPa, the 2000 Series is widely used in steam mains, heat exchangers, steam tracing systems, process equipment, food processing, pharmaceutical manufacturing, petrochemical plants, power generation, and other industrial steam systems.
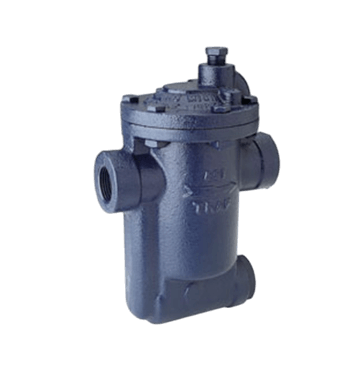
●The Armstrong 880 Series Inverted Bucket Steam Trap is engineered with Armstrong's proven inverted bucket operating mechanism to provide reliable condensate removal while automatically venting air and carbon dioxide from steam systems. Designed for long service life and dependable operation, it delivers excellent resistance to water hammer and minimizes steam loss.
●Featuring a cast iron body, stainless steel internal components, and an integrated strainer, the 880 Series enhances system reliability by reducing dirt-related failures and maintenance requirements. It is ideally suited for steam mains, steam tracing systems, heat exchangers, and a wide range of industrial steam process applications requiring efficient condensate drainage and energy savings.
●The Armstrong LD Series Free Lever Float Drain Trap is engineered to automatically discharge condensate from compressed air and industrial gas systems while preventing valuable gas loss. Utilizing Armstrong's proven free lever float mechanism, the valve responds precisely to condensate levels, providing reliable, continuous drainage with minimal maintenance.
●Available in 304L stainless steel and ASTM A105 forged steel constructions, the LD Series offers excellent corrosion resistance, high discharge capacity, long service life, and outstanding resistance to water hammer. With pressure ratings up to 6.9 MPa, it is widely used in compressed air systems, nitrogen service, natural gas applications, petrochemical plants, power generation, and industrial process facilities.
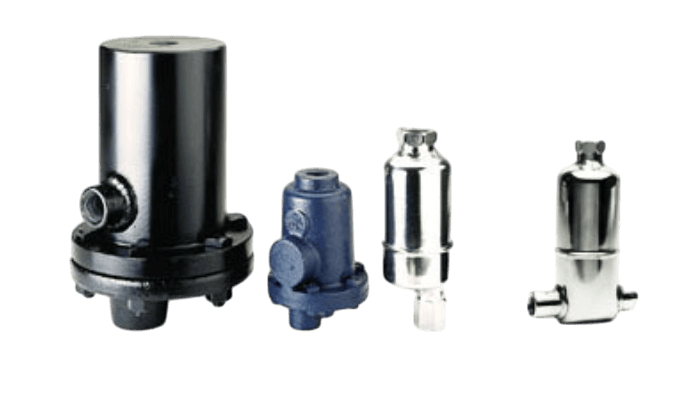
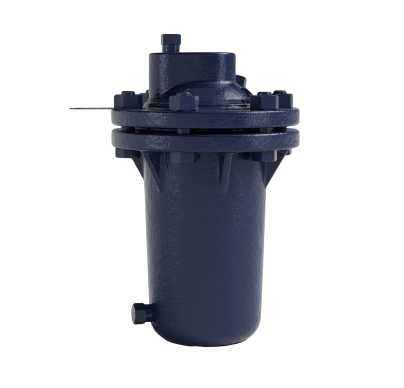
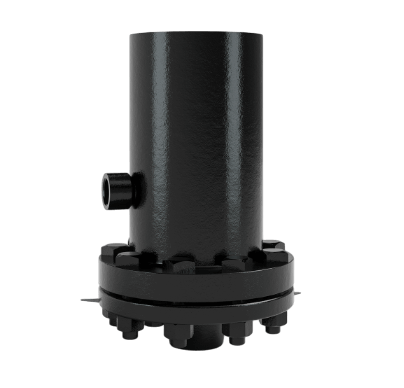
●The Armstrong BVSW Series Inverted Bucket Liquid drainer is engineered for industrial applications where condensate may contain heavy oil, sludge, or other contaminants. Its enlarged bucket vent and vent guide rod design allow liquid to discharge through the vent opening, helping to minimize clogging and ensure dependable condensate drainage under demanding operating conditions.
●Built on Armstrong's proven inverted bucket technology, the BVSW Series provides automatic condensate removal with reliable performance and reduced gas loss. Available in cast iron, forged steel, and cast steel constructions, it is suitable for operating pressures up to 4.5 MPa and is widely used in petrochemical plants, refineries, natural gas processing, industrial gas systems, and other contaminated condensate applications.
●The Armstrong HLS Series High Lift Lever Spring-Loaded Float Liquid drainer is specifically designed for automatic condensate removal from high-pressure gas systems while preventing valuable gas loss. Its high-lift lever and spring-loaded float mechanism provide dependable operation under high differential pressures and low specific gravity liquid conditions.
●Available in ASTM A105 forged steel, ASTM A182 F22 alloy steel, with selected models available in 316 stainless steel, the HLS Series delivers outstanding durability, corrosion resistance, and reliable condensate drainage for demanding industrial environments. With pressure ratings up to 25.5 MPa, it is widely used in natural gas processing, petrochemical plants, refineries, power generation, and industrial gas systems. The HLS Series is designed for gas applications and is not intended for steam service.
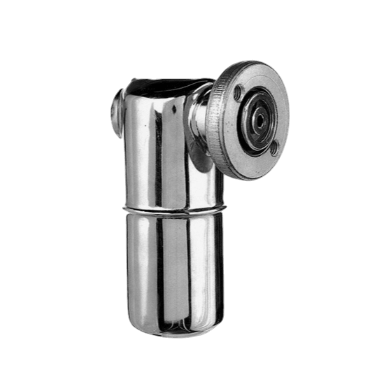
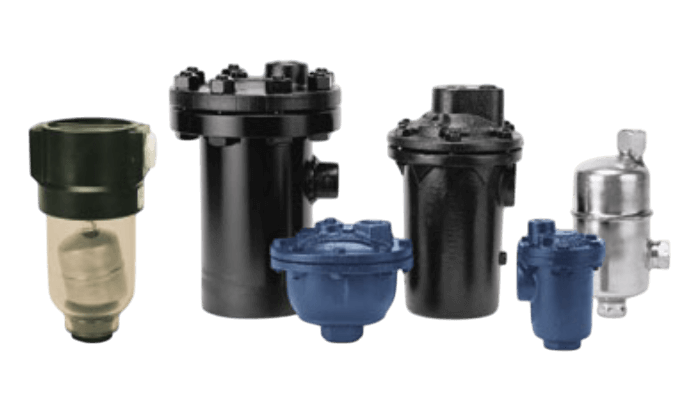
●Armstrong Free Lever Float Air Vents are designed to automatically and continuously remove entrained and trapped air from pressurized fluid systems during operation. Featuring a durable stainless steel body and a precision free lever float mechanism, these air vents provide reliable performance, excellent corrosion resistance, and long service life in demanding industrial environments.
●By eliminating air from steam, hot water, glycol, HVAC, and industrial cooling systems, Armstrong Air Vents improve heat transfer efficiency, reduce pump cavitation, minimize corrosion, and increase overall system reliability. They are widely used in industrial plants, HVAC systems, district heating, glycol circulation systems, data center liquid cooling, and petrochemical facilities.
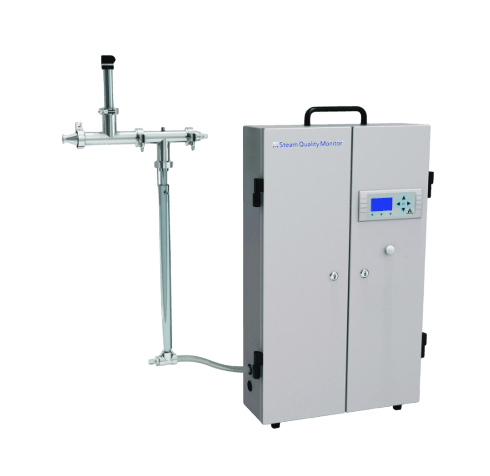
●Armstrong Steam QM®-3 is an advanced Clean Steam Quality Monitoring Solution designed to continuously measure steam dryness, superheat, and non-condensable gases (NCG) in clean steam systems. Engineered to support EN 285 sterilization requirements, Steam QM®-3 provides an automated alternative to conventional manual steam quality testing, delivering higher measurement accuracy, improved operational safety, and continuous trend analysis.
●Featuring plug-and-play installation, RS485/Modbus communication, and real-time monitoring capabilities, Steam QM®-3 enables pharmaceutical, biotechnology, medical device, food, and beverage facilities to verify steam quality, optimize sterilization performance, support GMP validation, and maintain consistent regulatory compliance.
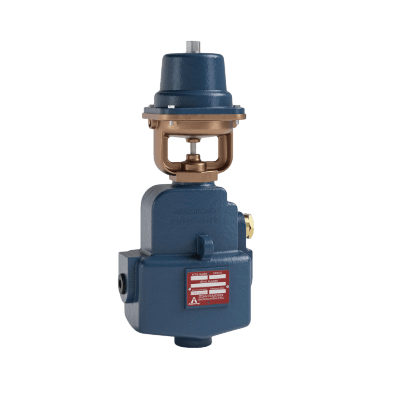
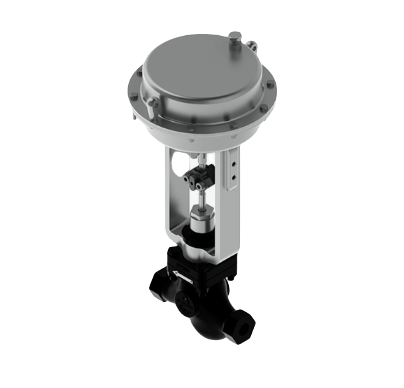
●Armstrong International has integrated the Leslie Controls® Flow Control product line and continues the trusted engineering, manufacturing expertise, and proven performance developed over decades. The renowned AEROFLOW®, D-Boy™, DLO™, K-Max™, DSE, DOS, and DOT™ control valve families are now exclusively supplied by Armstrong, providing reliable flow control solutions for power generation, oil & gas, chemical processing, food & beverage, pharmaceutical, pulp & paper, and other industrial industries.
●Resource from website of Armstrong International : https://armstronginternational.com/flow-control/
●Armstrong owns the exclusive rights to manufacture these Leslie Controls legacy brands and legacy brand OEM spare parts, adhering to the original specifications and drawings.
●Armstrong and its contractual representatives have exclusive rights to sell these legacy brands and support the install base.
●Armstrong is the exclusive owner of all technical details to include engineering and design of legacy Leslie Control Valve product lines.
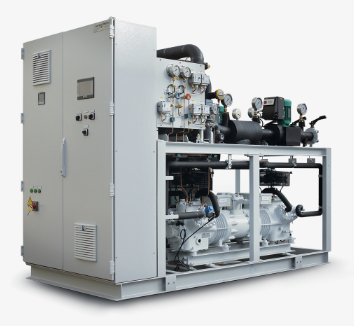
●Armstrong Industrial Heat Pump Systems are designed to recover low-grade waste heat from industrial processes and upgrade it into valuable high-temperature hot water through an advanced refrigeration cycle. These integrated systems provide efficient heating, cooling, and waste heat recovery while reducing fossil fuel consumption, lowering operating costs, and supporting thermal decarbonization. Custom-engineered solutions are available for food processing, pharmaceutical, chemical, paper, dairy, brewing, and other industrial applications.
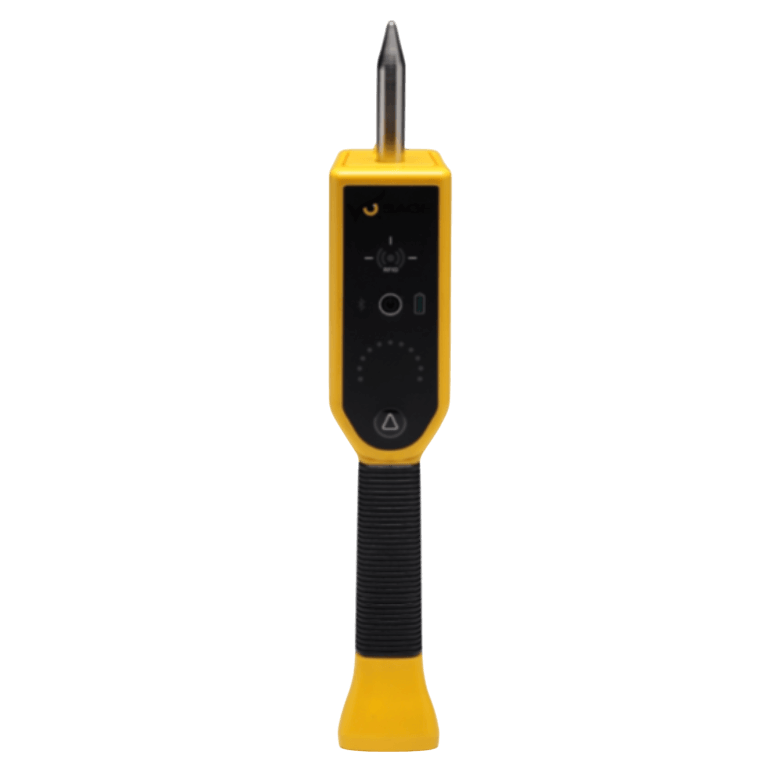
●The Armstrong SAGE UMT™ Steam Trap Tester is an intelligent wireless inspection device designed to evaluate steam trap performance using ultrasonic sensing, infrared temperature measurement, RFID identification, and Bluetooth communication.
●Integrated with the Armstrong SAGE® Energy Management Platform, the UMT automatically uploads inspection data, maintains asset history, and generates maintenance and energy performance reports. This enables faster inspections, improved steam trap reliability, reduced steam losses, lower energy consumption, and predictive maintenance for industrial steam systems. It is an ideal solution for digital steam trap management and Industrial IoT applications.


Fluid Control & Intelligent System Solutions
Your Trusted Partner for Reliable and Efficient Solutions.
Steam & Condensate recovery Liquid drainer (air trap) Fluid control Flow meter Heat pump system Safety valve Ancillary products Intelligent monitoring systems Hot water system Humidifier
Tel: +886 39892577/+81 7038715929
Email: info@shunjien.com
WhatsApp: +81 7038715929
Open: Monday to Friday 8:30-17:30
© SJ Machinery Co., Ltd. Copyright All Rights Reserved
We value your privacy