Steam & Condensate recovery Liquid drainer (air trap) Fluid control Flow meter Heat pump system Safety valve Ancillary products Intelligent monitoring systems Hot water system Humidifier
Hospital Applications Hydrogen Refueling Stations & Hydrogen Pipeline Applications Application
Pamphlet/Catalog Download Technical article Frequently Asked Questions News
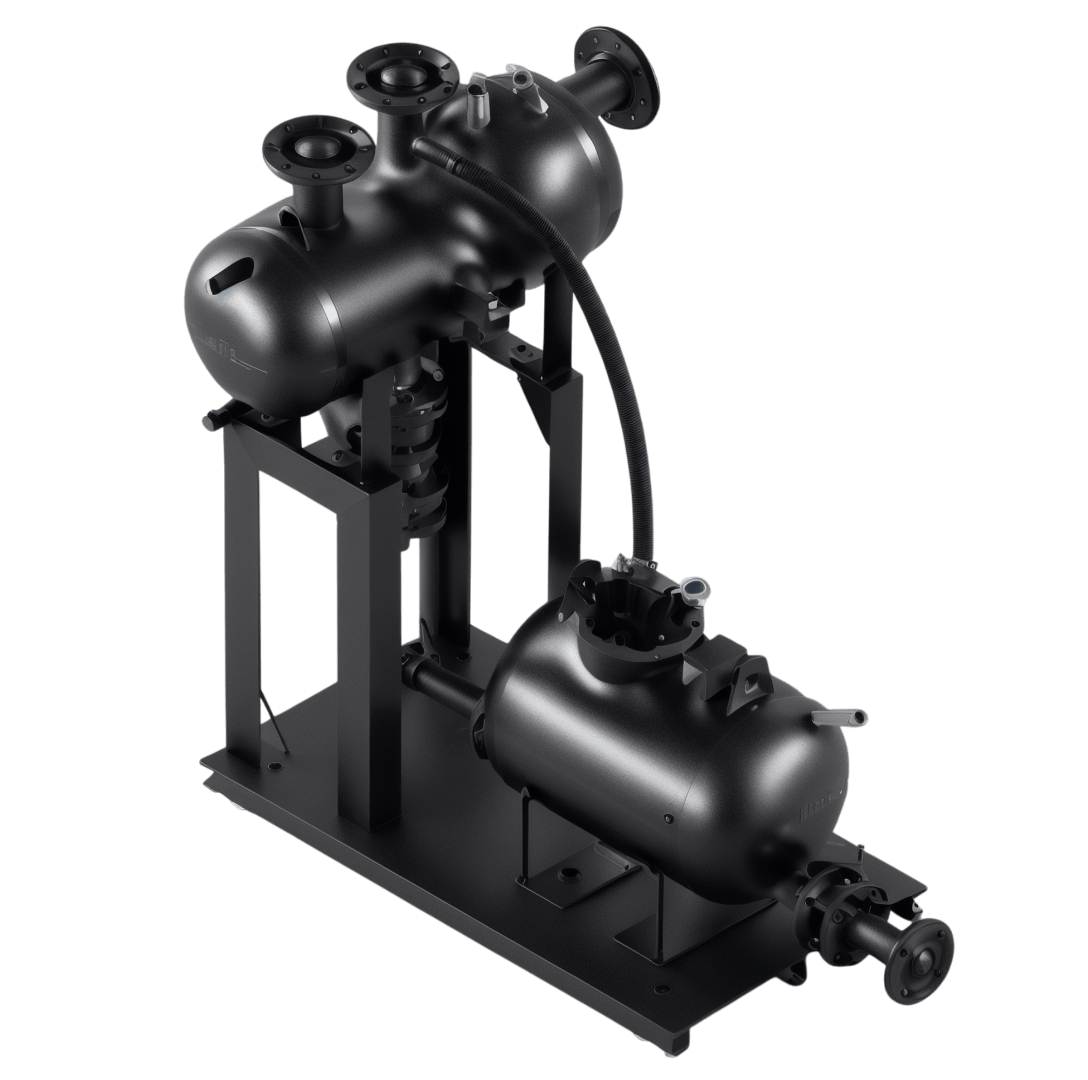
●The Armstrong Condensate Return Unit is a complete packaged condensate recovery system that integrates a condensate receiver tank, condensate pumps, and control components into a compact, factory-assembled unit.
●Available in single-, dual-, triple-, and quad-pump configurations, the system efficiently returns hot condensate to the boiler feedwater system, reducing fresh water consumption, fuel costs, and water treatment expenses while improving overall steam system efficiency.
●Factory-engineered and pre-assembled, the unit minimizes on-site installation time, enhances operational reliability, and provides an economical solution for condensate recovery in food processing, chemical, pharmaceutical, biotechnology, electronics, textile, and other industrial steam applications.


Fluid Control & Intelligent System Solutions
Your Trusted Partner for Reliable and Efficient Solutions.
Steam & Condensate recovery Liquid drainer (air trap) Fluid control Flow meter Heat pump system Safety valve Ancillary products Intelligent monitoring systems Hot water system Humidifier
Tel: +886 39892577/+81 7038715929
Email: info@shunjien.com
WhatsApp: +81 7038715929
Open: Monday to Friday 8:30-17:30
© SJ Machinery Co., Ltd. Copyright All Rights Reserved
We value your privacy