

- Homepage
- Brand
-
Products
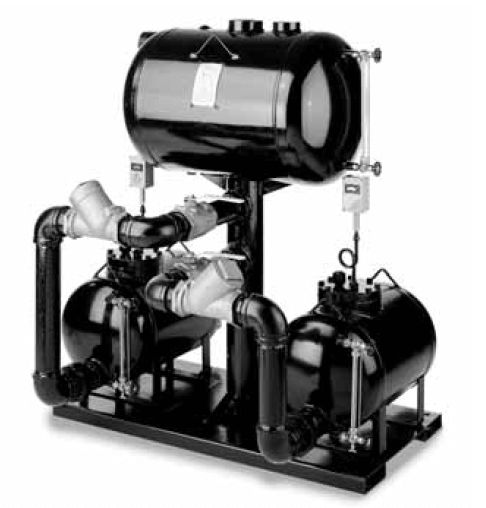
Steam & Condensate recovery Liquid drainer (air trap) Fluid control Flow meter Heat pump system Safety valve Ancillary products Intelligent monitoring systems Hot water system Humidifier
-
Case Study
Hospital Applications Hydrogen Refueling Stations & Hydrogen Pipeline Applications Application
-
Resources
Pamphlet/Catalog Download Technical article Frequently Asked Questions News
- Contact