Steam & Condensate recovery Liquid drainer (air trap) Fluid control Flow meter Heat pump system Safety valve Ancillary products Intelligent monitoring systems Hot water system Humidifier
Hospital Applications Hydrogen Refueling Stations & Hydrogen Pipeline Applications Application
Pamphlet/Catalog Download Technical article Frequently Asked Questions News
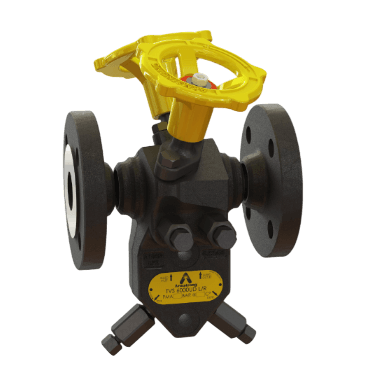
●The Armstrong TVS All-in-One Steam Trap Station is a fully integrated 5-in-1 and 10-in-1 steam trap assembly that combines dual isolation valves, an integrated strainer, blowdown valves, test valves, and a universal connector into a single compact, space-saving solution for steam trapping applications.
●Note: No bypass function is provided. Please consult us for applications requiring continuous 24/7/365 operation without system shutdown.
●Designed to simplify installation and maintenance, the TVS allows steam traps to be replaced without modifying existing piping, significantly reducing downtime and maintenance costs. Its modular design minimizes field piping, improves operational safety, and enhances steam system reliability.
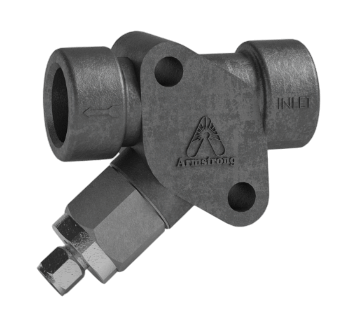
●The Armstrong IS Universal Connector is designed to simplify the installation and maintenance of steam traps. Its modular design allows steam traps to be replaced quickly without disconnecting the pipeline, significantly reducing maintenance time and system downtime.
●Available with an integrated 304 stainless steel strainer, blowdown valve, and multiple connection options including threaded, socket weld, and flanged configurations, the IS improves steam trap protection and enhances steam system reliability. It is compatible with Armstrong 2000, FT-4000, CD-3300, AB-2000, and TT-2000 Series steam traps, making it an ideal solution for industrial steam systems.
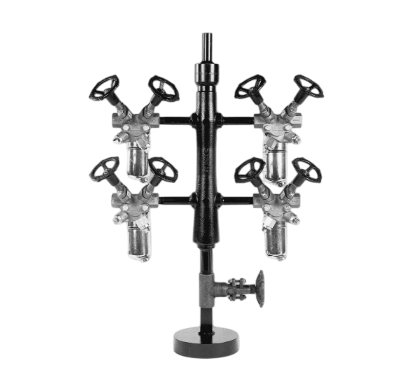
●The Armstrong CCA (Condensate Collection Assembly) and CCAF Series are engineered to collect condensate from multiple TVS 4000 steam traps into a single condensate header. This modular assembly simplifies piping layouts, reduces installation time, lowers material costs, and improves overall steam system reliability.
●Manufactured with a heavy-duty ASTM A105 forged steel header, the CCA/CCAF Series is rated for 4.2 MPa at 427°C, making it suitable for high-pressure industrial steam systems. It is widely used in power generation, petrochemical, chemical processing, food processing, pharmaceutical manufacturing, electronics, and other industrial condensate recovery applications.
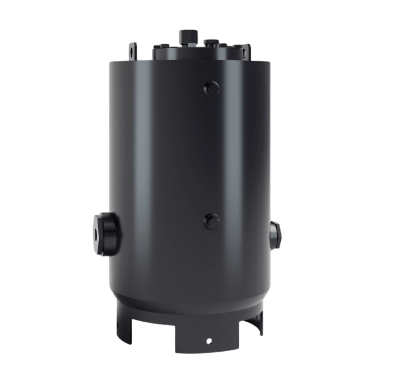
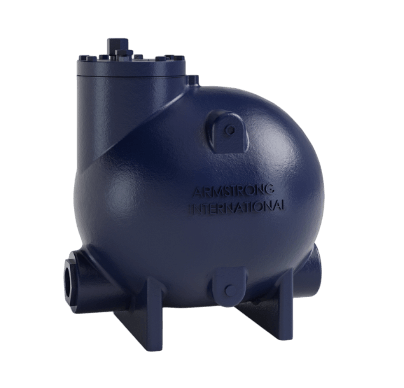
●The Armstrong Double Duty™ Pumping Trap combines the functions of a steam trap and a mechanical condensate pump into one compact unit. It automatically switches between steam trapping and condensate pumping according to receiver pressure, ensuring reliable condensate removal even when differential pressure is insufficient.
●Powered entirely by steam, the Double Duty™ operates without electricity, making it an ideal solution for installations where electrical power is unavailable or undesirable. It effectively eliminates condensate backup, reduces water hammer, improves heat transfer efficiency, and maximizes condensate recovery.
●Designed for demanding industrial steam systems, the unit is suitable for heat exchangers, process equipment, HVAC systems, food processing, pharmaceutical plants, chemical facilities, and other steam applications requiring dependable condensate removal. The pressure vessel is manufactured to ASME Section VIII standards for safety and reliability.
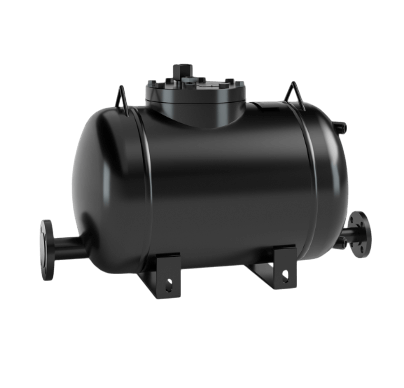
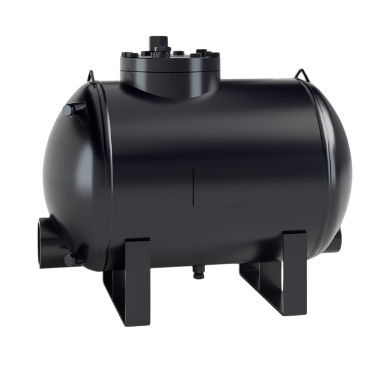
●The Armstrong PT series Pumping trap is a non-electric horizontal condensate recovery pump designed to operate using steam or compressed air. It provides reliable condensate removal in applications where gravity drainage or conventional electric pumps are ineffective due to high back pressure or insufficient differential pressure.
●The PT series Pumping trap efficiently returns hot condensate to the boiler feedwater system, reducing energy loss, fresh water consumption, and water treatment costs while preventing condensate backup and water hammer. Constructed with a heavy-duty steel pressure vessel and stainless steel internal components, it delivers long service life, dependable performance, and minimal maintenance for demanding industrial steam applications.
●The Armstrong PT series Pumping trap is a non-electric horizontal condensate recovery pump designed to operate using steam or compressed air. It provides reliable condensate removal in applications where gravity drainage or conventional electric pumps are ineffective due to high back pressure or insufficient differential pressure.
●The PT series Pumping trap efficiently returns hot condensate to the boiler feedwater system, reducing energy loss, fresh water consumption, and water treatment costs while preventing condensate backup and water hammer. Constructed with a heavy-duty steel pressure vessel and stainless steel internal components, it delivers long service life, dependable performance, and minimal maintenance for demanding industrial steam applications.
●The Armstrong PT series Pumping trap is a non-electric horizontal condensate recovery pump designed to operate using steam or compressed air. It provides reliable condensate removal in applications where gravity drainage or conventional electric pumps are ineffective due to high back pressure or insufficient differential pressure.
●The PT series Pumping trap efficiently returns hot condensate to the boiler feedwater system, reducing energy loss, fresh water consumption, and water treatment costs while preventing condensate backup and water hammer. Constructed with a heavy-duty steel pressure vessel and stainless steel internal components, it delivers long service life, dependable performance, and minimal maintenance for demanding industrial steam applications.
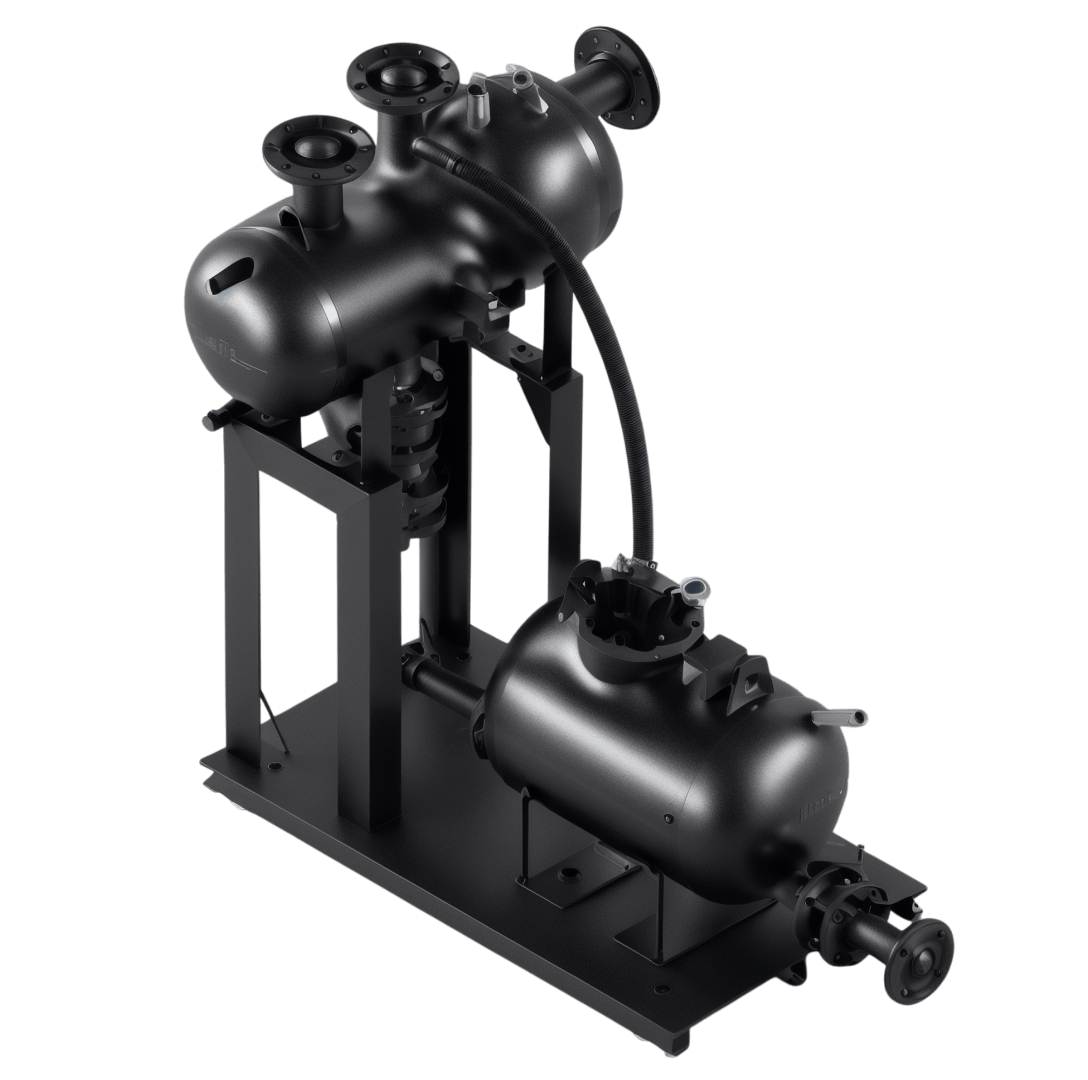
●The Armstrong Condensate Return Unit is a complete packaged condensate recovery system that integrates a condensate receiver tank, condensate pumps, and control components into a compact, factory-assembled unit.
●Available in single-, dual-, triple-, and quad-pump configurations, the system efficiently returns hot condensate to the boiler feedwater system, reducing fresh water consumption, fuel costs, and water treatment expenses while improving overall steam system efficiency.
●Factory-engineered and pre-assembled, the unit minimizes on-site installation time, enhances operational reliability, and provides an economical solution for condensate recovery in food processing, chemical, pharmaceutical, biotechnology, electronics, textile, and other industrial steam applications.
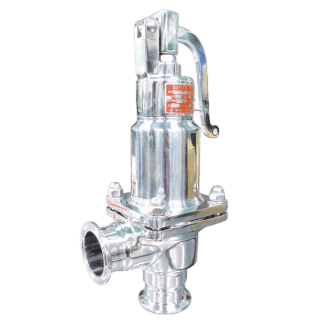
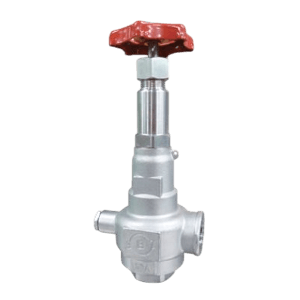
●The MIHANA Sanitary Safety Valve SVSC is specifically designed for food, beverage, pharmaceutical, and biotechnology sterilization processes. Featuring a Tri-Clamp (Clamp) connection, the valve provides a hygienic, crevice-free installation that helps prevent fluid or product residue from remaining inside the piping system.
●Designed to meet the demanding requirements of sanitary applications, the SVS Series delivers reliable overpressure protection, excellent sealing performance, and easy maintenance, making it an ideal choice for clean process systems.
●Suitable for liquid and steam service. Not for gas applications.
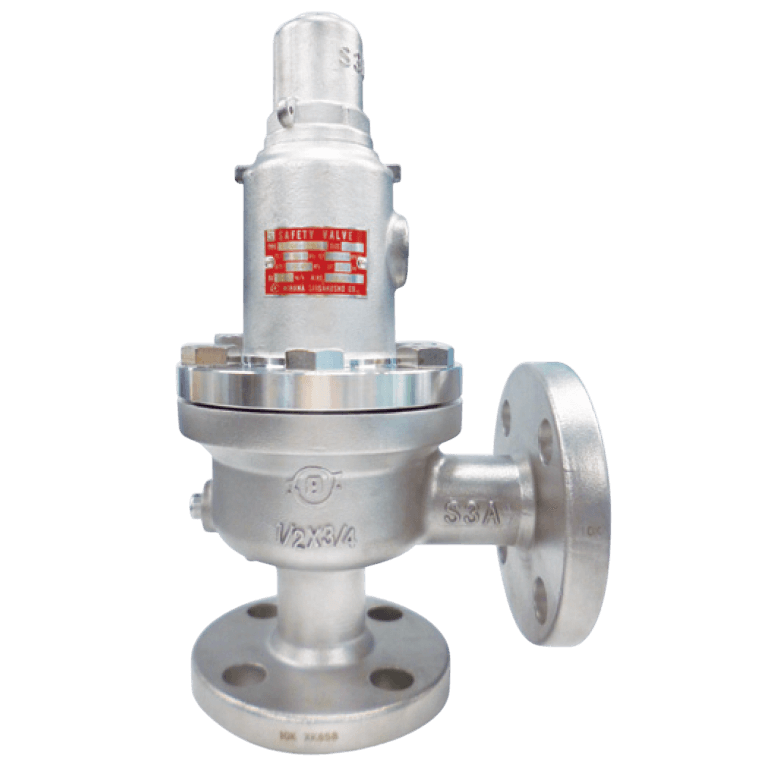
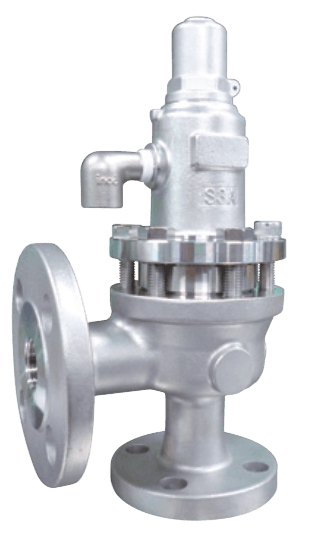
●The MIHANA SB101 Flanged Low-Lift Type Safety Valve is available with JIS 10K and ANSI flange connections.
●The MIHANA SD10X Lowlift Type Safety Valve is specifically engineered for high-pressure pipeline applications, with a maximum operating pressure of 59 MPa. Manufactured with an SCS13A stainless steel valve body, the SD10X Series has been widely adopted in hydrogen refueling station applications.
●
●Developed for demanding high-pressure environments, the SD10X incorporates MIHANA's proprietary precision seat lapping technology to achieve outstanding sealing performance. It provides reliable overpressure protection while maintaining zero leakage across the entire operating pressure range, making it an ideal solution for hydrogen, high-pressure gas, and industrial process systems.
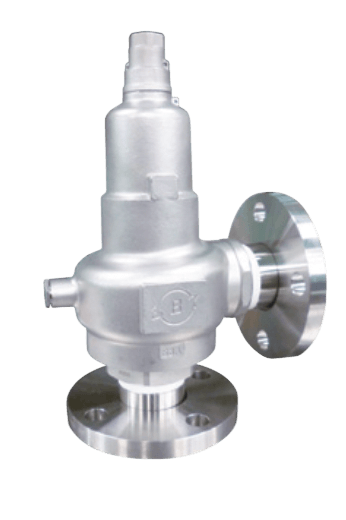
●The MIHANA KANTAK Flanged Lowlift Type Safety Valve features a stainless steel construction, excellent corrosion resistance, convenient lift testing, and reliable overpressure protection for industrial gas and process fluid systems.
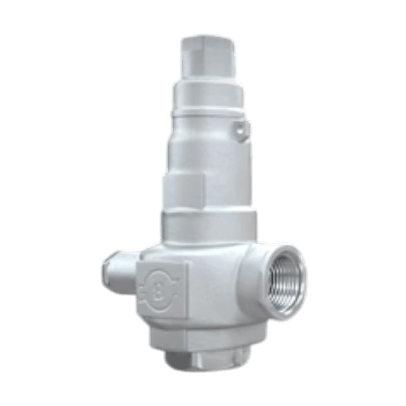
●The MIHANA Lowlift Safety Relief Valve HKANTAE is specifically designed for pump pressure relief and liquid system protection. It is widely used to protect pumps and piping systems from overpressure and is not suitable for steam service.
●
●To enable precise pressure adjustment, the HKANTAE Series features an ergonomic round adjustment handle. Its compact design provides a comfortable grip while requiring minimal operating space, allowing for smooth and accurate pressure setting. Engineered for reliable performance, the HKANTAE Series offers dependable overpressure protection for a wide range of industrial liquid applications.
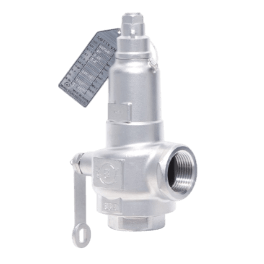
●The MIHANA LKANTAE-S Lowlift Type Safety Relief Valve is specifically engineered for liquid service applications. Manufactured with a SCS13A (equivalent to ASTM CF8 / SS304 cast stainless steel) valve body, it is suitable for a wide range of liquids compatible with SS304 materials.
●
●Designed to provide accurate pressure relief, reliable sealing performance, and long-term durability, the LKANTAE-S Series is an ideal solution for protecting liquid process systems in various industrial applications.
●Designed for applications with fluctuating back pressure. MIHANA's proprietary lapping technology overcomes the common leakage issues associated with conventional bellows safety valves, delivering reliable long-term sealing performance.


Fluid Control & Intelligent System Solutions
Your Trusted Partner for Reliable and Efficient Solutions.
Steam & Condensate recovery Liquid drainer (air trap) Fluid control Flow meter Heat pump system Safety valve Ancillary products Intelligent monitoring systems Hot water system Humidifier
Tel: +886 39892577/+81 7038715929
Email: info@shunjien.com
WhatsApp: +81 7038715929
Open: Monday to Friday 8:30-17:30
© SJ Machinery Co., Ltd. Copyright All Rights Reserved
We value your privacy